Why Choose the Carlo Gavazzi MNFR15 Photoelectric Sensor?
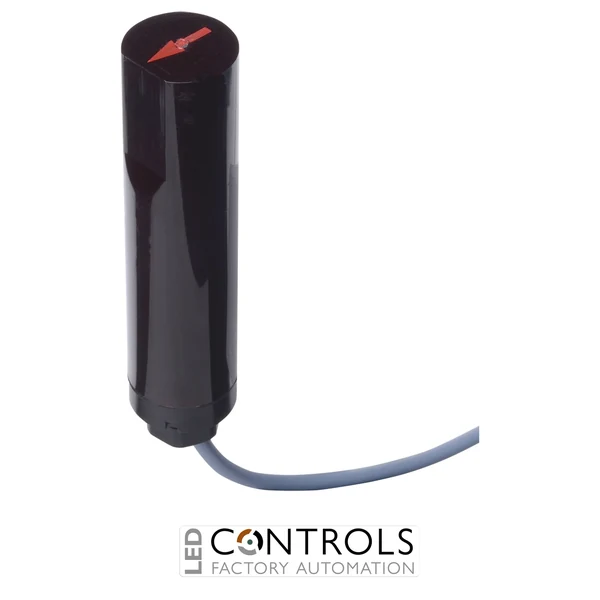
The Carlo Gavazzi MNFR15 is a high-performance through-beam photoelectric receiver designed for reliable object detection in industrial automation and harsh operating environments. Part of the Carlo Gavazzi MNF photoelectric sensor series, it provides accurate optical detection when used with a compatible S142 amplifier system.
This receiver is designed for separate amplifier operation and uses modulated infrared light technology to provide excellent immunity against ambient light interference. Its compact 20 mm diameter polycarbonate housing and robust construction make it suitable for demanding industrial sensing applications.
With a 15 m sensing range, IP66/IP67 protection and a straight optical receiver design, the MNFR15 is ideal for reliable detection in automation equipment, production machinery and industrial monitoring systems.
Key Advantages
- Reliable through-beam photoelectric receiver for industrial detection.
- 15 m sensing range for flexible installation distances.
- High immunity to ambient light interference.
- Compact 20 mm cylindrical housing for space-saving installation.
- IP66/IP67 protection suitable for harsh environments.
- Designed for use with Carlo Gavazzi S142 amplifier systems.
Key Features
- Carlo Gavazzi MNF photoelectric sensor series.
- Through-beam receiver design.
- 15 m rated operating distance.
- Infrared modulated light detection.
- 20 mm diameter polycarbonate housing.
- Straight optical axis configuration.
- High penetration power for reliable detection.
- Suitable for water, dust and steam environments.
- Compatible with S142 amplifier series.
Reliable Optical Detection for Industrial Automation
Through-beam photoelectric sensors provide accurate object detection by separating the light emitter and receiver, allowing reliable sensing across longer distances and challenging industrial environments. The Carlo Gavazzi MNFR15 receiver works together with a compatible amplifier to provide dependable detection performance.
The MNF series is designed for applications requiring strong optical performance, resistance to ambient light and reliable operation in environments where dust, moisture and industrial contamination may be present.
Typical Applications
- Industrial automation equipment.
- Production and packaging machinery.
- Object presence detection.
- Material handling systems.
- Machine monitoring applications.
- Industrial process control systems.