Why Choose the Carlo Gavazzi MOFT20-5 Photoelectric Sensor?
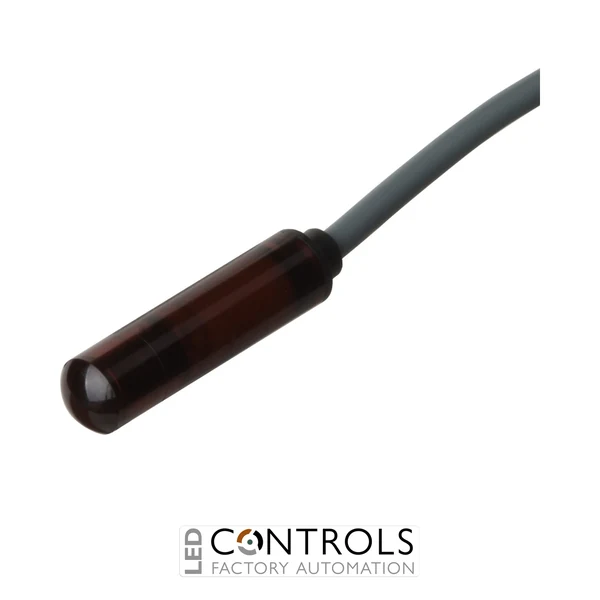
The Carlo Gavazzi MOFT20-5 is a reliable photoelectric through-beam sensor designed for accurate object detection in industrial automation, machine control and material handling applications. Part of the Carlo Gavazzi MOF photoelectric sensor series, it provides dependable optical sensing performance for demanding industrial environments.
The MOFT20-5 uses photoelectric technology to detect the presence or absence of objects without physical contact. Its compact cylindrical design, flexible AC/DC supply capability and combined NO + NC output configuration make it suitable for integration into a wide range of industrial control systems.
With a 30 m sensing range, AC/DC power supply compatibility, NO + NC output contacts and integrated cable connection, the Carlo Gavazzi MOFT20-5 provides dependable object detection for automation equipment and industrial machinery.
Key Advantages
- Through-beam photoelectric sensing technology for reliable long-distance detection.
- 30 m sensing range suitable for industrial automation applications.
- NO + NC output configuration provides flexible control integration.
- AC/DC supply compatibility supports versatile installation requirements.
- Non-contact optical detection eliminates mechanical wear.
- Compact industrial design for easy machine integration.
Key Features
- Carlo Gavazzi MOF photoelectric sensor series.
- Through-beam (transmitter/receiver) sensing principle.
- 30 m operating sensing distance.
- NO + NC output configuration.
- AC/DC operating supply.
- Cable connection version.
- Suitable for object presence and position detection.
- Designed for industrial automation systems.
Reliable Optical Detection for Industrial Automation
Photoelectric sensors such as the Carlo Gavazzi MOFT20-5 provide fast and accurate object detection by using light-based sensing technology. Through-beam sensors are particularly suited to applications requiring reliable detection over longer distances or where precise object positioning is required.
The MOF series offers compact and dependable sensing solutions for machine builders, OEM equipment manufacturers and industrial automation engineers requiring consistent detection performance in production environments.
Typical Applications
- Industrial automation equipment.
- Material handling and conveyor systems.
- Packaging machinery.
- Production line object detection.
- Machine positioning and control systems.
- Industrial process monitoring.