Why Choose the Carlo Gavazzi PH18CNR65NAT1SA Retro-Reflective Photoelectric Sensor?
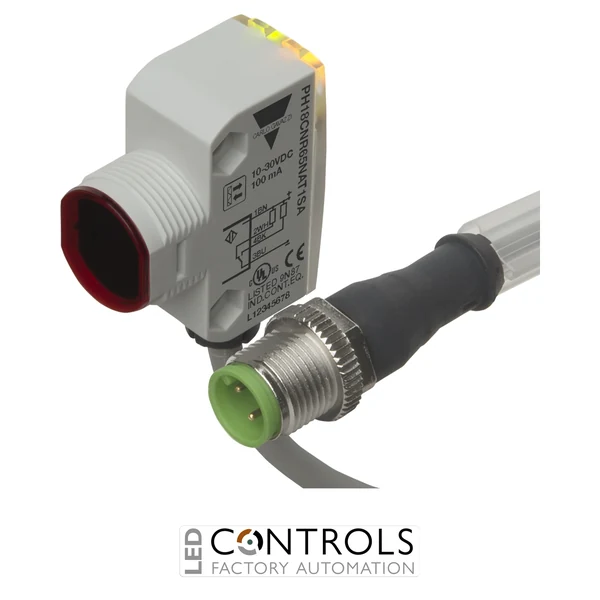
The Carlo Gavazzi PH18CNR65NAT1SA is a robust retro-reflective photoelectric sensor designed for reliable non-contact object detection in industrial automation and control applications. As part of the Carlo Gavazzi PH18 square M18 photoelectric sensor series, it provides accurate sensing performance in a rugged housing suitable for demanding industrial environments.
This sensor combines retro-reflective optical technology, a compact square M18 design and flexible transistor outputs to provide dependable detection of objects, packages and materials. The PH18 series is engineered for machine builders requiring reliable switching, simple installation and compatibility with PLC-based automation systems.
With a sensing range of 6.5 m, NPN NO + NC outputs and a pigtail cable connection, the PH18CNR65NAT1SA is ideal for detecting moving objects across conveyors, packaging equipment and automated production machinery.
Key Advantages
- Durable retro-reflective photoelectric sensor for industrial automation.
- 6.5 m sensing range suitable for medium-distance object detection.
- NPN NO + NC transistor outputs provide flexible control integration.
- Square M18 housing enables secure machine mounting.
- Pigtail connection simplifies installation and maintenance.
- Reliable operation in industrial production environments.
Key Features
- Carlo Gavazzi PH18 photoelectric sensor series.
- Retro-reflective detection principle.
- 6.5 m rated sensing distance.
- NPN output with NO + NC switching configuration.
- 10–30 V DC supply voltage.
- Visible red modulated light source.
- Adjustable sensitivity.
- Compact square M18 threaded housing.
- Pigtail cable connection for flexible wiring.
Reliable Object Detection for Industrial Automation
Photoelectric sensors such as the Carlo Gavazzi PH18CNR65NAT1SA detect objects without physical contact by transmitting light towards a reflector and monitoring the returned signal. Retro-reflective technology provides reliable object detection for automated handling and production processes.
The PH18 series is designed for automation engineers and OEM machine builders requiring rugged sensors with dependable switching performance. Its M18 housing, flexible outputs and compact design support straightforward integration into industrial systems.
Typical Applications
- Industrial conveyors and material handling systems.
- Packaging and production machinery.
- Object counting and position detection.
- Assembly automation equipment.
- Machine control and monitoring systems.
- OEM industrial automation applications.