Why Choose the Carlo Gavazzi MNFT15 Photoelectric Sensor?
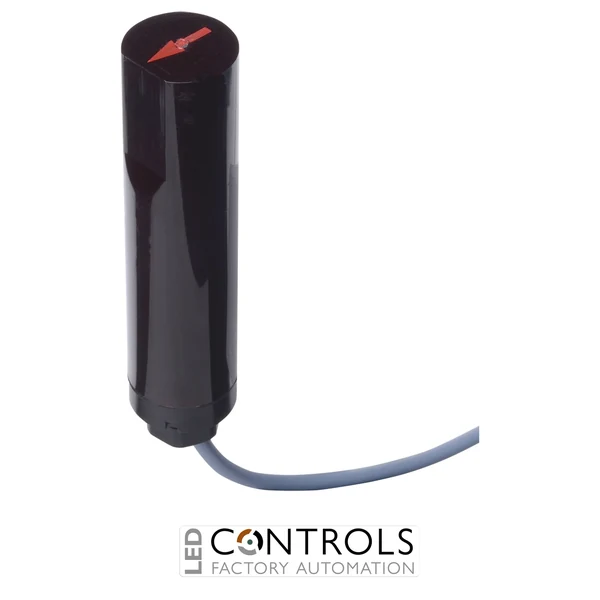
The Carlo Gavazzi MNFT15 is a reliable through-beam photoelectric transmitter designed for accurate object detection in industrial automation and sensing applications. As part of the Carlo Gavazzi MNF photoelectric sensor series, it provides a dependable infrared light source for use with compatible receivers and amplifier systems.
This transmitter features a compact 20 mm cylindrical housing with an 8° optical aperture, providing precise alignment and reliable operation in demanding industrial environments. Its separate emitter and receiver arrangement allows long-distance detection where consistent sensing performance is required.
With a 15 m sensing range, cable connection and robust industrial construction, the MNFT15 is suitable for automated machinery, production equipment and industrial monitoring systems requiring dependable through-beam detection.
Key Advantages
- Reliable through-beam photoelectric transmitter for industrial detection.
- 15 m sensing range for flexible machine installation.
- 8° optical aperture supports accurate beam alignment.
- Compact 20 mm cylindrical housing for space-saving installation.
- Infrared technology provides dependable object detection.
- Designed for use with compatible Carlo Gavazzi receiver and amplifier systems.
Key Features
- Carlo Gavazzi MNF photoelectric sensor series.
- Through-beam transmitter design.
- 15 m rated operating distance.
- 8° optical beam aperture.
- 20 mm diameter housing.
- Infrared modulated light source.
- Cable-connected sensor design.
- Suitable for industrial object detection applications.
- Designed for reliable operation with separate receiver systems.
Reliable Optical Detection for Industrial Automation
Through-beam photoelectric sensors provide accurate detection by separating the transmitter and receiver, allowing reliable sensing across longer distances and in challenging industrial conditions. The Carlo Gavazzi MNFT15 provides the infrared transmission element required for dependable optical detection systems.
The MNF series is designed for industrial applications requiring consistent sensing performance, compact installation and reliable operation in automated machinery and production environments.
Typical Applications
- Industrial automation equipment.
- Production and packaging machinery.
- Object presence detection.
- Material handling systems.
- Machine monitoring applications.
- Industrial process control systems.